Minnox exceeds all state, regional, national and international emission standards for NOx and CO
In the United States, installation of a Minnox system may allow your company to receive valuable emissions credits which you can sell to other companies in your area.
Widely recognized as an engineering breakthrough, Minnox received the coveted DSM Environmental Technology Award.
Minnox is also a marvel of simplicity and safety, meeting or exceeding all international codes and regulations
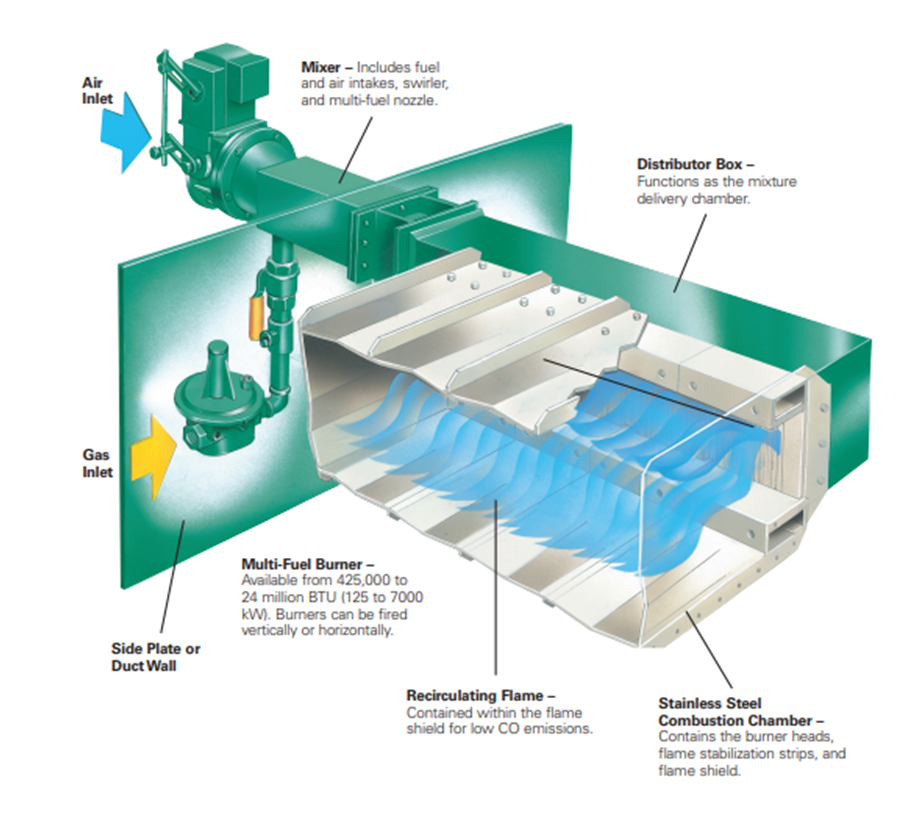
The patented Minnox burner design utilizes a premixed gas/air mixture with excess air. The result is a cooler flame (2200° F; 1200° C) which produces an extremely low NOx discharge. What’s more, a recirculating flame geometry actsto significantly reduce CO emissions. Not only is the air outside your plant cleaned up…so is the air inside to create a saferand healthier workplace.
Consider these additional user benefits:
Allows you to use direct heat–– as opposed to less efficient indirect heating––with no performance penalty. Product discoloration or taste contamination often associated with traditional direct heating systems are a thing of the past.
All Minnox systems are custom engineered to meet your specific production and installation requirements.
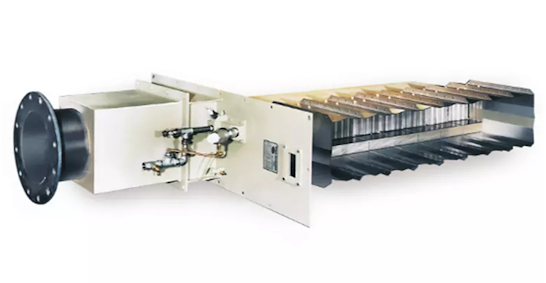
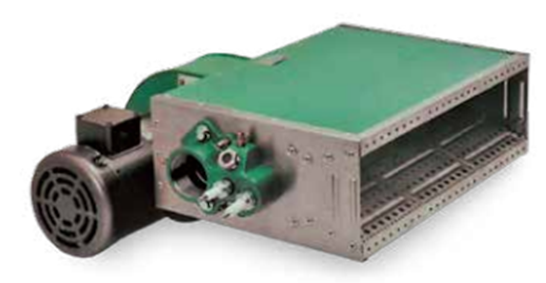
Packaged convenience. Minnox systems are typically supplied with the burner, mixer and supply manifold mounted into a duct section or as a side plate for insertion into existingprocess ductwork.